English
Request a Quote
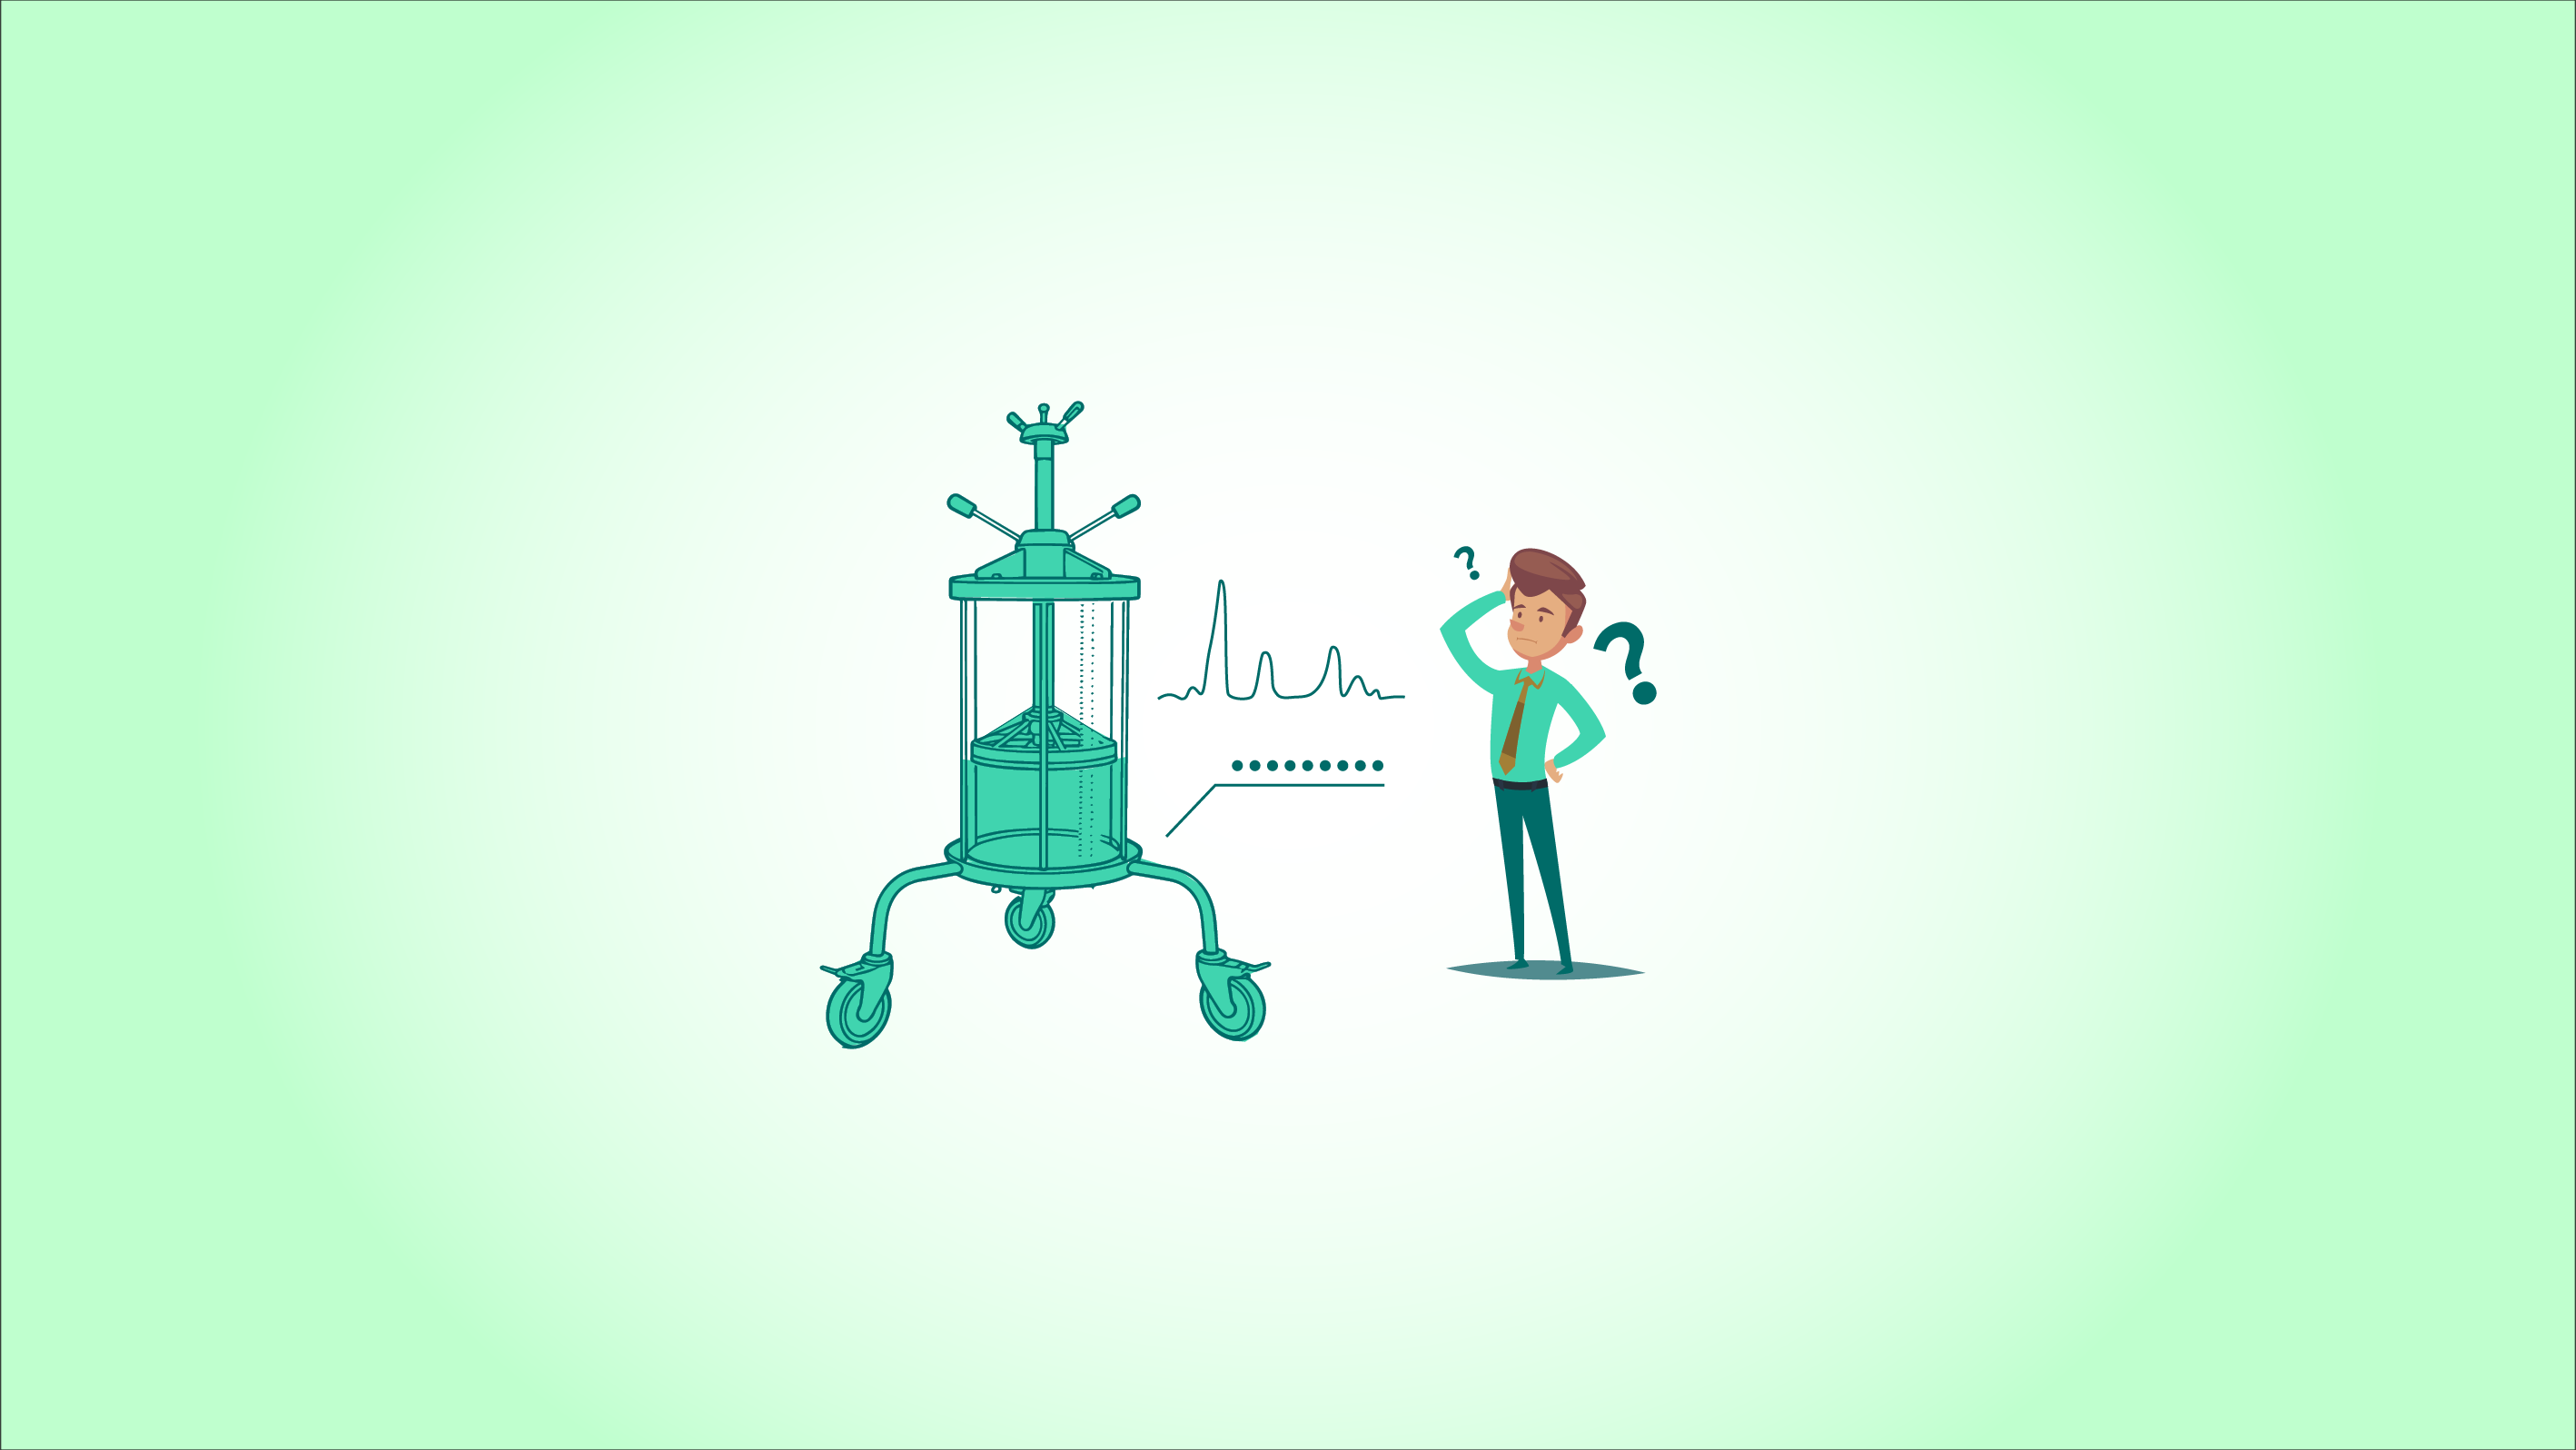
In chromatography process development, nearly every team goes through a similar stage: laboratory results are stable, with good purity and yield performance, but once the process is transferred to pilot or manufacturing scale, deviations begin to appear:
• Changes in elution peak position
• Reduced impurity clearance capability
• Increased variability or even significant drop in yield
• Abnormal column pressure or reduced column efficiency
These phenomena are often simply attributed to “scale-up issues.” However, if we probe further, a more critical question emerges: scale-up does not change the process logic—so why do the outcomes change?
In laboratory settings, a process is typically understood as a set of “operating parameters”:
• pH
• Salt concentration
• Flow rate
• Loading capacity
During scale-up, these parameters are often directly and strictly “linearly transferred” or proportionally reproduced. However, from an engineering perspective, a process is not solely determined by these surface-level parameters; instead, it is governed by a deeper set of underlying variables:
• Mass transfer processes
• Flow distribution
• Local concentration gradients
• Solid–liquid interfacial behavior
When equipment size changes, these variables do not necessarily scale linearly. Therefore, fundamentally speaking, scale-up is not simply a change in volume, but a change in the physical state of the system.
The essence of a chromatographic process lies in the transfer of molecules from the mobile phase into the resin pores, followed by interaction within the stationary phase. This process is highly dependent on mass transfer efficiency.
At laboratory scale:
• Column diameter is small
• Flow distribution is uniform
• Mass transfer path length is short
Molecules can quickly reach adsorption equilibrium.
At larger scale:
• Column diameter increases
• Flow distribution becomes more complex
• Mass transfer path length is extended
Even when the same “residence time” is maintained, the actual mass transfer efficiency may still change, leading to:
• Deviation of dynamic binding capacity (DBC) from laboratory data
• Shift in adsorption/desorption equilibrium
• Narrowing of the separation window
This is why, in some projects, a situation arises where a “sufficient residence time” at laboratory scale no longer holds true after scale-up.
In small-scale chromatography columns, fluid typically passes relatively uniformly through the packed bed. However, as column diameter increases, flow distribution becomes more complex:
• Non-uniform inlet distribution
• Local variations in flow velocity
• Reduced wall effects
These factors lead to non-uniform utilization of the packed bed:
• Some regions become overloaded
• Some regions are underutilized
In such cases, even if overall operating parameters remain unchanged, the actual process performance can change significantly, for example:
• Peak broadening or tailing
• Unstable impurity separation
• Decreased column efficiency
Therefore, from an engineering perspective, non-uniform flow distribution is one of the key sources of process variation during scale-up.
During scale-up, another often overlooked factor is the uniformity of sample loading.
At laboratory scale:
• Small column diameter and short flow paths
• Relatively uniform sample concentration distribution
At manufacturing scale:
• Larger column diameter and longer flow paths
• More difficult to achieve uniform feed distribution during loading
This can lead to the formation of local concentration gradients, causing different regions of the packed bed to experience uneven loading. When local regions approach or exceed their binding capacity, the following may occur:
• Early breakthrough
• Co-elution of impurities
• Enhanced non-specific binding
These effects are often difficult to observe at laboratory scale but become amplified and more apparent after scale-up.
In addition to the column itself, the overall system can also introduce variability in scale-up performance, for example:
• Increased system dead volume
• Changes in tubing length
• Differences in mixing efficiency
• Inconsistent gradient formation
These factors can affect:
• Gradient accuracy
• Elution behavior
• Peak shape performance
At laboratory scale, these variables are often relatively small and therefore easily overlooked. However, in manufacturing systems, their impact becomes increasingly pronounced.
When all the factors described above are considered together, a key conclusion emerges: scale-up deviations are often not caused by differences in nominal parameters, but by changes in the underlying physical reality that those parameters represent.
For example:
• Identical flow rate ≠ identical mass transfer conditions
• Identical residence time ≠ identical adsorption equilibrium
• Identical loading ≠ identical local loading distribution
This is why relying solely on laboratory-scale parameters for scale-up can, in some cases, lead to inconsistent or non-reproducible performance.
From an engineering practice perspective, improving scale-up success rates relies on shifting from “parameter replication” to “mechanistic consistency.”
First, during the laboratory stage, attention should be paid not only to separation performance, but also to mass transfer and kinetic characteristics. For example, residence time variation studies can be used to evaluate the system’ s sensitivity to mass transfer limitations.
Second, in scale-up design, flow distribution and bed structure should be considered in an integrated manner, including appropriate column height, packing quality, and distributor design.
In addition, sample loading and concentration distribution must be controlled to avoid nonlinear effects caused by local overloading.
Finally, necessary verification should be performed at the pilot scale, rather than directly scaling from laboratory to manufacturing scale.
From laboratory to industrial production, scale-up of chromatographic processes is not a simple replication of operating parameters, but rather a test of whether the underlying basis of process control remains valid.
At small-scale development, processes are typically established under relatively ideal flow distribution, shorter system pathways, and lower scale-up complexity. However, upon scale-up, factors such as column wall effects, system dead volume, flow distribution, and pressure-flow constraints may all change, thereby affecting mass transfer, retention behavior, and the separation window. The key to industrial scale-up is not to ensure that all parameters appear identical, but to verify whether the truly governing variables of separation (e.g., residence time, bed height, and bed utilization state) remain comparable across scales.
Therefore, in process development, rather than pursuing a single set of locally optimal conditions, it is more important to identify early the system’s sensitivity to key variables: whether the process is approaching mass transfer limitations, whether separation depends on a specific level of column efficiency, and whether impurity clearance shifts with bed height or system conditions. Only when these mechanistic relationships are fully understood does scale-up cease to be empirical extrapolation and become an engineering process that is verifiable, predictable, and controllable.
Nov
13
Nov
06
Oct
23


.png)
.png)
.png)
.png)